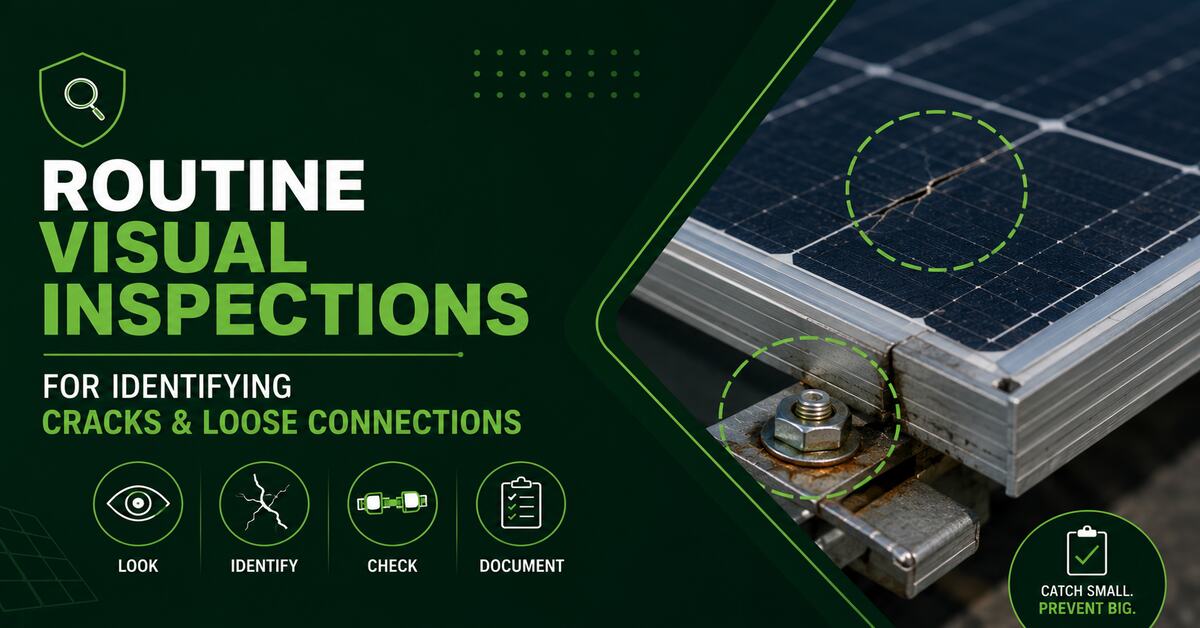
Routine visual inspections for identifying cracks and loose connections are systematic, non-destructive evaluations used to detect physical stress, material separation, and fastener failure. This procedure requires angled lighting, surface cleaning, and strict documentation to differentiate superficial wear from active structural or electrical degradation before catastrophic breakdown occurs.
Key Facts / At a Glance
- Target zones: Inspections must prioritize heat-affected zones (HAZ) near welds, structural corners, and high-vibration mountings.
- Illumination rules: Angled lighting (10–15 degrees to the surface) is mandatory to cast shadows inside hairline fractures.
- Fretting indicators: Fine metal powder residue around bolted joints indicates active friction and lost clamp load.
- Method limitations: Visual Testing (VT) cannot confirm subsurface crack depth; it requires secondary Non-Destructive Testing (NDT) like dye penetrant for validation.
- Safety mandates: Tactile “wiggle” tests on electrical connections strictly require OSHA Lockout/Tagout (LOTO) and zero-energy verification.
Before You Start: Inspection Parameters
- Total Time: 15–45 minutes per standard industrial asset.
- Difficulty: Moderate (Requires blueprint literacy and component familiarity).
- Estimated Cost: $50–$300 for professional-grade visual testing tools.
- Required Tools:
- LED flashlight (minimum 500 lumens, adjustable beam).
- Magnification loupe (10x to 50x optical zoom).
- Inspection mirrors or articulating borescope.
- Lint-free rags and non-corrosive degreaser.
- Scale indicator (for photo reference).
- Prerequisites: Active LOTO permits, Arc Flash PPE (if inspecting electrical cabinets), and historical maintenance logs.
How Do You Prepare for an Inspection?
Preparation determines the accuracy of your findings. You must isolate the equipment to ensure safety, strip away environmental contaminants that hide defects, and review historical data to know exactly where the asset is statistically most likely to fail.
Step 1: Establish Zero Energy and Safety Controls
Isolate the equipment from all power sources before your hands or tools enter the inspection plane. Apply Lockout/Tagout (LOTO) locks, verify zero energy using a calibrated multimeter, and secure tool tethers if working at heights.
- Specifics: Maintain a minimum boundary distance according to NFPA 70E standards if panels remain energized for thermal visual checks.
- Success Checkpoint: You will know this step is complete when the equipment cannot physically be activated and all stored kinetic or pneumatic energy is bled off.
- Common Mistake: Relying solely on a disconnected switch without verifying zero voltage with a meter, leading to arc flash exposure during tactile checks.
Step 2: Clean and Expose the Surface
Wipe away grease, heavy dust, and pooling fluids that mask material separation. Use lint-free rags and an approved industrial degreaser to expose the bare metal or painted joint.
- Specifics: Clean an area extending at least 2 inches (50mm) past the suspected high-stress zone.
- Success Checkpoint: The surface is dry, matte, and free of any debris that could be misconstrued as a shadow or fracture under harsh lighting.
- Common Mistake: Using abrasive wire brushes on soft metals (like aluminum), which can smear the metal and physically push material over a hairline crack, hiding it entirely.
How Do You Identify Structural Cracks?
Identifying structural cracks relies heavily on manipulating light and understanding stress mechanics. You are looking for breaks in surface continuity that propagate outward from points of maximum tension or vibration.
Step 3: Apply Angled Lighting to High-Stress Zones
Shine your flashlight at a low, oblique angle (10 to 15 degrees) across welded joints, structural corners, and rigid mountings. This technique forces any surface anomaly to cast a distinct shadow, highlighting defects invisible under direct, overhead light.
- Specifics: Move the light source in a 180-degree arc around the joint. Cracks only cast shadows when the light hits them perpendicular to their length.
- Success Checkpoint: You will detect a jagged, dark line that remains stationary as you move the light, distinct from the surrounding surface texture.
- Common Mistake: Using a wide-flood beam directly above the surface, which blasts light into the crack and washes out the critical shadows.
Step 4: Map Secondary Surface Markers
Look for indirect evidence of cracking when the fracture itself is too tight to see. Watch for paint flaking in a linear pattern, active rust bleeding (red/brown streaks tracking out from a weld), or moisture seeping from a seemingly solid joint.
- Specifics: Use a 10x magnification loupe to inspect the edges of flaking paint. If the metal beneath shows a dark, hair-thin separation, a crack is actively expanding.
- Success Checkpoint: You have successfully traced a rust trail back to its exact origin point on a seam or weld bead.
- Common Mistake: Assuming rust bleeding is just surface oxidation. Rust streaks originating from a pinpoint or joint line almost always indicate internal moisture trapped by a crack.
What Indicates a Loose Connection?
Loose connections betray themselves through physical displacement, vibration wear, and thermal degradation. Detecting them requires a combination of visual marker verification and safe tactile testing.
Step 5: Inspect Fasteners for Displacement and Fretting
Check mechanical joints for missing bolts, shifted alignment, or displaced washers. Look for torque witness marks (stripes of anti-sabotage lacquer across the bolt head and base metal); if the two halves of the stripe no longer align, the bolt has backed out.
- Specifics: Scan the base of fasteners for “fretting”—a fine white, gray, or brown metallic powder. This powder is created when a loose bolt microscopically vibrates and grinds against the base material.
- Success Checkpoint: You instantly identify compromised fasteners by spotting misaligned witness marks or accumulated metal dust.
- Common Mistake: Re-torquing a bolt without documenting it first. If you tighten it immediately, you destroy the evidence of a recurring vibration issue.
Step 6: Perform the Wiggle Test on De-energized Points
Once LOTO is confirmed and electrical panels are completely dead, gently manipulate plugs, wire cables, and joint fittings by hand.
- Specifics: Apply no more than 2–3 pounds of lateral force. Terminals should feel absolutely rigid. Check for discolored plastic, blistering on wire insulation, or melted terminal blocks, which signify high electrical resistance caused by a loose connection arcing under load.
- Success Checkpoint: You physically confirm whether a connection is secure or if it slips, wobbles, or exhibits excessive play.
- Common Mistake: Wiggling wires too aggressively, which can inadvertently break fragile, aged insulation or damage the terminal seating.
How Should You Document Findings?
Documentation transforms a physical observation into actionable maintenance data. A visually identified defect is useless if the repair crew cannot locate it or understand its severity.
Step 7: Capture Standardized Photographic Evidence
Take two photographs of every defect: one wide-angle shot for environmental context, and one extreme close-up (macro) shot.
- Specifics: Always place a physical scale indicator (a ruler or coin) directly next to the crack or loose bolt in the macro shot to establish exact proportions.
- Success Checkpoint: A third-party technician can look at your photos and immediately navigate to the exact component on the factory floor.
- Common Mistake: Taking blurry macro photos without a reference point, making it impossible to tell if a crack is two millimeters or two inches long.
Step 8: Assign Severity Metrics
Log the precise component ID and categorize the problem by risk level using a standardized matrix. This dictates the maintenance scheduling priority.
| Severity Level | Definition | Required Action | Example Finding |
| Critical | Imminent risk of catastrophic failure or severe safety hazard. | Immediate shutdown and emergency repair. | Expanding crack on a load-bearing crane weld. |
| Major | Significant degradation; failure likely within the current maintenance cycle. | Schedule repair within 7–14 days. | Melted insulation on a high-voltage terminal. |
| Minor | Early signs of wear; no immediate threat to operation. | Monitor and log for next inspection. | Slight misalignment of a witness mark on a non-critical mount. |
Common Inspection Mistakes and Fixes
Even experienced practitioners misinterpret visual data. Acknowledging the limitations of human sight and surface conditions is critical for accurate reporting.
- Mistake: Confusing Scratches with Cracks. Deep manufacturing tool marks can mimic hairline fractures.
- How to fix it: Look at the ends of the line under a loupe. Tool marks terminate bluntly; fatigue cracks branch out like lightning bolts or taper to an microscopic point. When in doubt, use a liquid dye penetrant to confirm.
- Mistake: Ignoring the “Halo” Effect on Electrical Panels. Inspectors often look only at the wire itself.
- How to fix it: Look at the metal cabinet wall directly behind the terminal block. A loose connection will often leave a faint, dark soot “halo” on the backplane from micro-arcing.
- Mistake: Skipping Hard-to-Reach Areas. Inspectors naturally favor components at eye level.
- How to fix it: Mandate the use of articulating borescopes or inspection mirrors for the blind sides of motors, pumps, and structural I-beams.
Variations by Asset Type
No two environments degrade equipment exactly the same way. You must adjust your visual inspection parameters based on the asset’s primary stressor.
High-Vibration Machinery
For assets like industrial centrifuges, crushers, or heavy screens, calendar-based inspections fail. Inspections must be condition-based or tied to operating hours. Focus 80% of your time on mounting feet, isolation springs, and heavy-duty fastener fretting.
High-Voltage Electrical Enclosures
Physical tactile testing is frequently impossible due to arc flash hazards when panels cannot be immediately powered down. In these scenarios, visual inspections rely entirely on thermal discoloration (blued copper, charred plastics) and require supplementation with infrared (IR) thermography tools to detect the heat generated by loose connections under load.
Frequently Asked Questions
How often should routine visual inspections be performed?
Inspection frequency depends on the asset’s criticality and environment. High-vibration or load-bearing equipment requires weekly visual checks, while static infrastructure may only require monthly or quarterly assessments.
Can visual inspections detect subsurface cracks?
No. Visual Testing (VT) is strictly limited to surface-breaking defects. If a crack originates internally and has not yet breached the surface material, visual inspections will miss it. Secondary methods like ultrasonic testing are required for subsurface flaws.
What is rust bleeding and what does it indicate?
Rust bleeding appears as red or brown streaks radiating outward from a joint or painted surface. It indicates that moisture has penetrated a microscopic crack or loose joint, corroded the unprotected metal inside, and seeped back out.
Why is powder residue present around bolted joints?
This fine metal dust is the result of fretting corrosion. When a bolt loses its clamping force, the two metal surfaces micro-vibrate against each other, grinding away the material and leaving a visible powder trail.
What tools are essential for detecting loose wire connections?
Beyond standard LOTO gear, you need a high-lumen flashlight to spot darkened or melted insulation, a magnification loupe to check for micro-arcing soot, and insulated screwdrivers to safely conduct tactile wiggle tests on de-energized blocks.